Engineering Next-Generation Retroreflective Workwear, Ultra-Lightweight Protective Shells, and High-Visibility Solutions for Global B2B Industrial Procurement.
Direct-from-factory reflective vests, lightweight jackets, and ANSI-compliant protective workwear optimized for industrial durability and wearer comfort.
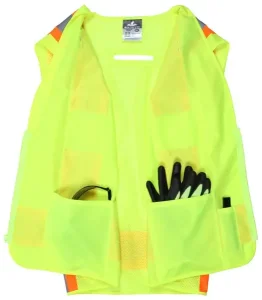
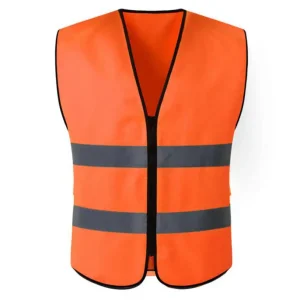
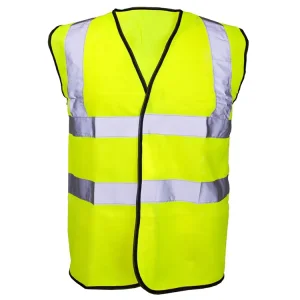
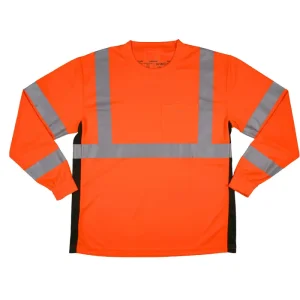
Analysis of market demands, ergonomic shifts, and regulatory drivers transforming high-visibility safety clothing procurement worldwide.
Modern industrial safety standards demand a transition from heavy 300D PVC-coated jackets to ultra-lightweight, high-tensile 75D-150D micro-polyester fabrics. Industrial procurement teams are prioritizing moisture vapor permeability to mitigate heat stress while maintaining 100% compliance with ANSI/ISEA 107-2020 and EN ISO 20471 Class 2/3 requirements.
Cross-border supply chains require precise adherence to regional safety frameworks. North American markets enforce ANSI Class 2/3 minimum retroreflective area, European importers require EN ISO 20471 certified fluorescent dyes with specific chromaticity coordinates, and Australian operations demand UPF 50+ UV protection integrated into lightweight AS/NZS 4602.1 garments.
Sourcing from tier-1 China manufacturers guarantees direct oversight of raw material specifications. From automated micro-taping of seams to high-precision laser pattern cutting, direct OEM integration minimizes supply chain friction, shortens lead times, and allows extensive private-label customization at competitive unit pricing.
A rigorous examination of fabric deniers, retroreflective tape technologies, and breathability ratings engineered for maximum industrial protection.
By bonding 100% micro-denier polyester outer shells to microporous TPU (Thermoplastic Polyurethane) backings, our factory produces lightweight Hi-Vis jackets weighing less than 180 GSM while providing a Hydrostatic Head waterproof rating exceeding 10,000mm H2O and a Moisture Vapor Transmission Rate (MVTR) of over 5,000 g/m²/24h. This eliminates the traditional trade-off between stormproof isolation and internal thermal regulation.
| Garment Architecture | Base Material & Fabric Weight | Retroreflective Technology | Waterproof & Breathability | Primary Industrial Sector |
|---|---|---|---|---|
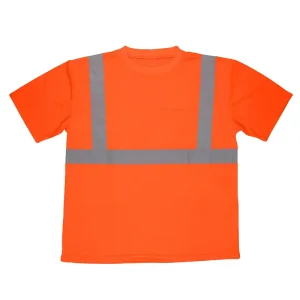
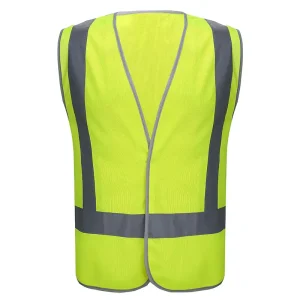
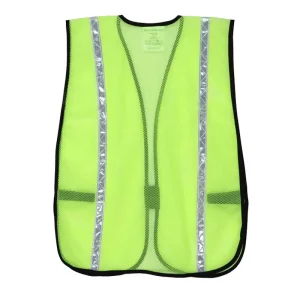
| Summer Ultra-Light Mesh Shell | 110-120 GSM 100% Polyester Open Tricot Mesh | Class 2 Glass-Bead Hot-Melt Transfer Film (2") | Air Permeable Open-Weave Mesh Construction | Roadway Construction, Traffic Control, Warehousing |
| All-Weather Lightweight Windbreaker | 150D / 75D Mechanical Stretch Ripstop Polyester | Microprismatic High-Gloss Waterproof Tape | 10,000mm Hydrostatic Head / 5,000 MVTR Breathability | Civil Infrastructure, Railway Safety, Municipal Utilities |
| Technical Multi-Pocket Surveyor Jacket | 300D Oxford Polyester Shell with Lightweight Mesh Lining | High-Contrast Dual-Tone 3M™ Scotchlite™ Tape | DWR (Durable Water Repellent) Hydrophobic Finish | Civil Engineering, Site Inspection, Energy Exploration |
| FR-Treated Lightweight Softshell | 240 GSM Flame-Resistant Modacrylic / Cotton Blend | FR-Certified Segmented Heat Transfer Tape | NFPA 2112 / ASTM F1506 Flame Resistance Standard | Petrochemical Refineries, Offshore Drilling, Electrical Utilities |
Our OEM manufacturing facility ensures every batch of high-visibility garments undergoes accredited third-party lab testing for photometric and mechanical performance.
For North American distribution, garments are segmented into Type R (Roadway), Type P (Public Safety), and Type O (Off-Roadway). Our lightweight jackets meet strict surface area requirements for background material (minimum 775 sq inches for Class 2, 1,240 sq inches for Class 3) and retroreflective tape placement, guaranteeing 360-degree visibility against complex industrial backgrounds under headlight illumination.
European Union directives demand rigorous color fastness, chromaticity coordinates (Fluorescent Yellow, Fluorescent Orange-Red, Fluorescent Red), and luminance factors. Our reflective tapes undergo continuous testing to ensure retroreflectivity values remain above 330 cd/(lx·m²) even after 50 cycles of industrial laundering at 60°C, ensuring compliance for major EU tender bids.
Custom-engineered garment configurations designed for high-risk, specialized operational environments.
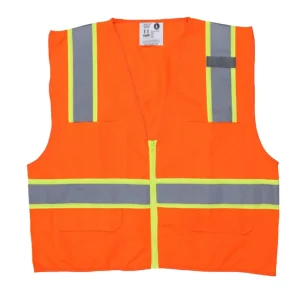
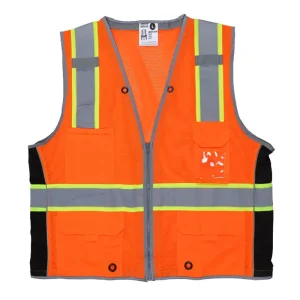
Features 5-point breakaway velcro architecture to prevent snag hazards near moving vehicles, ultra-light mesh underarm vents for heat mitigation, and high-contrast 4-inch lime/orange striping for maximum daytime visual pop.
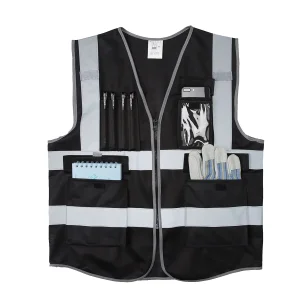
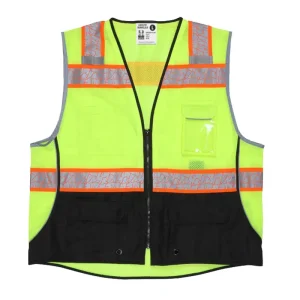
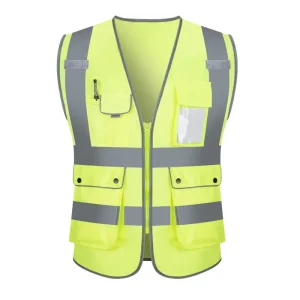
Configured with anti-FOD (Foreign Object Debris) zipper pull tabs, non-magnetic plastic hardware, clear PVC badge holders, dual radio mic loops, and EN 1149 anti-static conductive wiring for fueling zones.
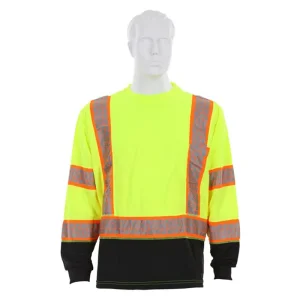
Ultra-flexible lightweight softshells with articulated sleeves, scuff-resistant dark lower hem panels to hide dirt and grease, and deep utility pockets optimized for handheld barcode scanners.
Inside our state-of-the-art production facility: How we deliver flawless safety apparel at scale.
Our factory utilizes Gerber computer-controlled automated laser cutters to ensure 0.1mm accuracy across all pattern pieces. Seams on lightweight waterproof jackets are sealed using high-pressure hot-air PU micro-taping machines, preventing water ingress at needle puncture points without adding bulk or weight to the garment body.
Every batch of fluorescent raw fabric is verified via Datacolor spectrophotometer to confirm delta-E color deviation remains under 1.0 within standard chromaticity boxes. Retroreflective tape samples undergo retroreflection coefficient tests ($R_A$) before and after abrasive wash testing to guarantee compliance prior to container loading.
Clear answers to technical specifications, minimum order quantities, customization, and international compliance.
Select from our complete range of certified protective apparel, shirts, waistcoats, and specialized safety accessories.