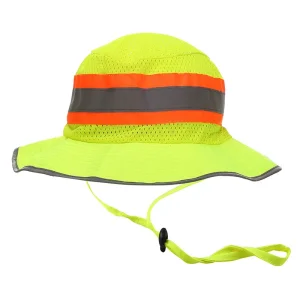
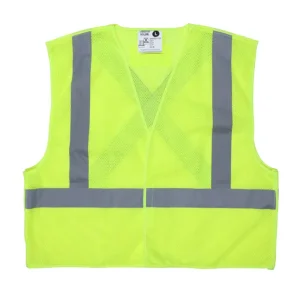
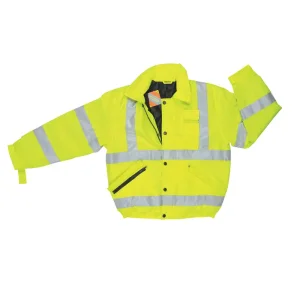
Explore our certified retroreflective gear engineered for severe working environments, construction zones, and high-risk utility sectors.
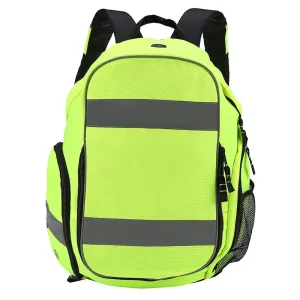
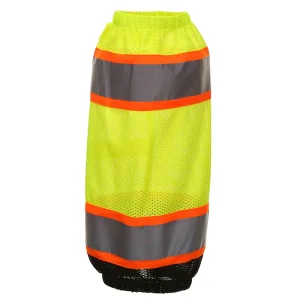
In modern industrial safety management, high-visibility (hi-vis) protective apparel has transcended traditional body-worn vests and jackets. As utility crews, railway line workers, highway construction technicians, emergency response personnel, and last-mile logistics fleets operate under complex 24/7 environmental conditions, carrying heavy tools and electronic gear has rendered conventional personal protective equipment (PPE) incomplete. When a field worker dons a standard non-reflective backpack over an ANSI/ISEA 107 or EN ISO 20471 certified safety vest, up to 40% of the retroreflective surface area on the back is completely obscured. This creates a dangerous visual blind spot, significantly increasing the probability of struck-by accidents involving heavy machinery, motor vehicles, or low-light work zone hazards.
To eliminate this critical safety bottleneck, global safety equipment procurement teams, OEM distributors, and government infrastructure agencies are rapidly shifting toward dedicated Hi-Vis Backpacks and Waterproof Reflective Backpack Covers. The international market for specialized high-visibility luggage and protective load-carrying equipment has experienced accelerated compounding growth, projected to expand at a CAGR of 6.8% over the next decade. Driven by stringent occupational health and safety (OHS) regulations across North America, the European Union, Australia, and the Asia-Pacific region, factory sourcing for compliant hi-vis load gear has transformed from a niche accessory category into a mandatory procurement requirement.
Strict enforcement of ANSI/ISEA 107-2020 (USA), EN ISO 20471:2013+A1:2016 (EU), and AS/NZS 1906.4:2010 (Australia) mandates uninterrupted 360-degree photometric visibility for night-shift and high-risk operational personnel.
The global boom in e-commerce, express courier services, and urban two-wheeler delivery riders has exponentially heightened demand for weatherproof, fluorescent neon rain covers featuring high-luster glass bead tape.
Telecommunications, electrical grid repair, rail infrastructure, and mining sectors demand dual-purpose gear: high tensile strength 600D/1680D ballistic polyester combined with certified retroreflective trim.
High-visibility gear performance depends on precise chromaticity, luminance factor, and retroreflective coefficient ($R_A$). Below is the architectural breakdown of certified fabric assembly.
The base fabric of professional hi-vis backpacks and covers must utilize specialized fluorescent dyestuffs capable of absorbing invisible ultraviolet (UV) light wavelengths from daylight and re-emitting them as visible light. Our manufacturing factory in Yongkang utilizes premium grade Fluorescent Yellow-Green (Pantone 13-0630 TN / 809C) and Fluorescent Orange-Red (Pantone 16-1356 TN / 804C) 100% polyester Oxford textiles. These fabrics undergo rigorous spectrophotometric testing to maintain luminance factors ($\beta \ge 0.70$ for yellow, $\beta \ge 0.40$ for orange) even after continuous UV exposure and harsh atmospheric weathering.
For night-time conspicuity, retroreflective elements send light beams back directly toward their originating light source (vehicle headlights). We incorporate two high-tier retroreflective tape architectures:
| Performance Spec | Standard Commercial Bag Cover | Industrial Hi-Vis Backpack Cover | Certified Tactical Hi-Vis Backpack |
|---|---|---|---|
| Base Fabric Density | 190T - 210D Polyester | 300D Oxford with PU Coating | 600D / 1680D Ballistic Oxford |
| Retroreflective Coefficient ($R_A$) | < 100 cd/(lx·m²) | ≥ 330 cd/(lx·m²) (Class 2) | ≥ 500 cd/(lx·m²) (Class 3 Grade) |
| Waterproof Hydrostatic Head | 1,000 - 1,500 mm | 5,000 - 8,000 mm | 10,000+ mm (Seam Sealed) |
| Tear Strength (ISO 13937-2) | < 15 N | ≥ 35 N | ≥ 85 N (Reinforced Box-Stitched) |
| Compliance Certification | Non-Certified / Fashion | EN ISO 20471 / ANSI 107 Class 2 | ANSI/ISEA 107 Class 3 / EN 343 4:4 |
As smart safety ecosystems and sustainable manufacturing gain global momentum, the OEM factory production line for hi-vis luggage is undergoing dynamic technological evolution.
Passive retroreflection depends entirely on vehicle lights shining directly onto the worker. Next-generation hi-vis backpacks incorporate flexible, waterproof, USB-rechargeable LED light pipes and Electroluminescent (EL) active illumination strips. This guarantees zero-light visibility in pitch-black subterranean utility tunnels, dark storage yards, and heavy fog where passive reflection falls short.
Multinational enterprise buyers and public sector procurement agencies now mandate strict ESG compliance. Our manufacturing roadmap integrates Global Recycled Standard (GRS) certified post-consumer recycled PET fabrics. By repurposing ocean-bound plastic bottles into ultra-durable 600D fluorescent yarn, we reduce carbon footprint by up to 45% without sacrificing tensile or photometric strength.
Occupational health studies indicate heavy load carrying causes chronic spinal fatigue among field technicians. Advanced hi-vis backpacks feature 3D breathable air-mesh back padding, sternum equalization straps, quick-release breakaway side buckles (to prevent entanglement in machinery), and integrated weight-distribution waist belts.
Moving beyond conventional needle-and-thread stitching, advanced factory production employs High-Frequency RF seam welding for TPU-coated backpack covers. Seamless construction eliminates needle puncture holes, providing 100% waterproof storm protection rated to IPX6 standard for torrential weather.
Different industries pose distinct environmental hazards. Our engineering factory provides custom-configured hi-vis backpack and cover solutions tailored to precise site demands.
Workplace Hazard: High-speed oncoming trains, severe wind turbulence, extreme night darkness, ballast dust.
Engineered Solution: Orange fluorescent high-contrast backpacks with double 3M Scotchlite 8912 silver retroreflective bands arranged in a V-chevron pattern on the rear panel. Includes heavy-duty lockable zipper slides and tool-loop MOLLE attachments.
Workplace Hazard: Proximity to high-velocity motor traffic, unpredictable driver behavior, low-light roadside work.
Engineered Solution: Dual-tone Lime/Orange ANSI Class 3 compliant backpack covers with elastic quick-fit tensioners, storm-drain water runoff channels, and transparent clear-window pockets for illuminated safety beacons.
Workplace Hazard: Saltwater spray corrosion, heavy crane cargo moving zones, high humidity, storm squalls.
Engineered Solution: Marine-grade TPU coated 600D Oxford backpacks featuring anti-corrosive plastic hardware, salt-spray resistant retroreflective trim, and internal waterproof laptop sleeves for field engineers.
Workplace Hazard: High frequency urban traffic interaction, heavy rain, rapid mounting and dismounting from two-wheelers.
Engineered Solution: Lightweight, compact fluorescent yellow backpack rain covers featuring high-stretch elastic border skirts, reflective logo branding, and anti-slip buckle straps securing the cover against high wind buffeting.
Workplace Hazard: Disaster site debris, dense smoke, off-grid forest navigation, extended search shifts.
Engineered Solution: Heavy-duty tactical hi-vis backpacks with hydration bladder ports, medical kit expansion modules, ID badge holders, and high-visibility glow-in-the-dark pull tabs for emergency access.
Workplace Hazard: Extreme dust build-up, confined space maneuvering, heavy machinery impact risks.
Engineered Solution: Anti-static and flame-retardant treated high-visibility backpack covers with wash-resistant micro-prismatic tape capable of retaining brightness under heavy dirt layer accumulation.
Yongkang Wow Safety Products Co., Ltd. brings over 15 years of continuous manufacturing excellence in reflective gear and high-visibility safety clothing.
Operating a modern 6,000 m² integrated production facility staffed by 150+ highly skilled textile workers, Yongkang Wow Safety Products Co., Ltd. serves procurement clients across 50+ countries. Our factory combines automated laser fabric cutting, ultrasonic sewing, high-frequency seam sealing, and specialized silk-screen/heat-transfer logo printing lines under one roof. Every batch of hi-vis backpacks and covers undergoes 100% optical and physical quality inspection prior to global dispatch.
We supply exact Pantone color-matched fluorescent polyester (Yellow, Orange, Red, Lime, Pink) with options for anti-UV, water-repellent (DWR), flame-retardant (NFPA 2112), and anti-static finishes.
Incorporate your company’s brand identity via industrial screen printing, reflective heat-transfer film, rubber badge molding, or high-density embroidery without compromising retroreflective certification zones.
For large-scale enterprise tenders, our R&D engineering unit develops customized backpack dimensions, internal organizer pockets, radio clips, and proprietary hardware fasteners tailored to contract specifications.
Clear technical answers to help safety officers, purchasing directors, and distributors make informed factory procurement decisions.
A Hi-Vis Backpack Cover is designed as an auxiliary safety enhancer to prevent backpacks from obscuring body-worn vests. While a certified Class 2 or Class 3 cover provides required background area and retroreflective coverage for the back torso, it should be used in conjunction with compliant high-visibility apparel to guarantee complete 360-degree front and side body visibility.
Under both ANSI/ISEA 107 and EN ISO 20471 standards, the minimum compliant width for primary retroreflective tape is 50mm (2 inches). For specialized high-contrast trim, 75mm (3-inch) bands featuring a silver retroreflective stripe center bordered by fluorescent orange or lime knit trim are frequently specified for railway and highway applications.
Standard reflective tapes degrade after 15 to 25 domestic washes. Our factory utilizes premium industrial-grade glass bead and micro-prismatic tapes engineered to withstand 50+ industrial laundering cycles at 60°C (140°F) while maintaining over 70% of initial coefficient values ($R_A > 230 \text{ cd}/(\text{lx}\cdot\text{m}^2)$).
For standard catalog products, our factory MOQ starts at 500 units per style. For custom fabric color dyeing, custom size grading, or tailored logo printing, MOQ ranges between 1,000 and 2,000 units. Customized OEM pre-production samples are completed within 5 to 7 working days upon design approval.
Yes. Our universal backpack covers feature 360-degree perimeter elastic drawstrings combined with dual adjustable cross-body compression straps. This dual-securing mechanism allows a single cover size to snugly fit gear volumes ranging from 20L daypacks to 45L tactical tool backpacks without wind flapping or slippage.
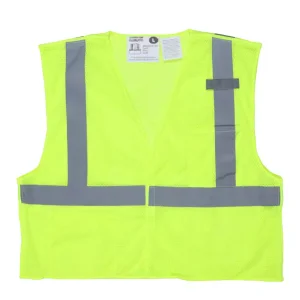
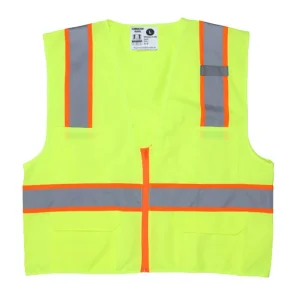
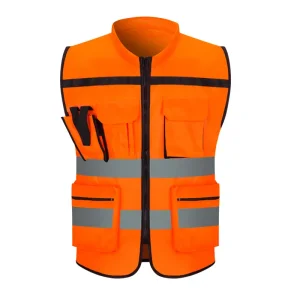
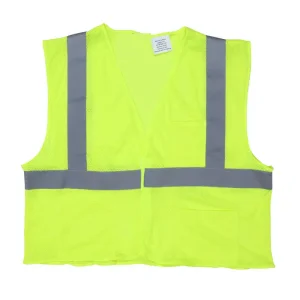
Explore our extended manufacturing lineup of high-visibility vests, rainwear, jackets, and specialized industrial accessories.
Partner directly with China's leading certified high-visibility safety clothing & reflective product factory. Over 15 years of OEM/ODM expertise supplying B2B distributors, government contracts, and enterprise fleets worldwide.