Engineered to comply with Class D/N daytime and night-time high-visibility requirements across Australian worksites.
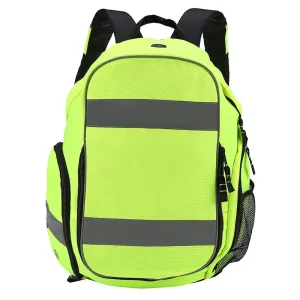
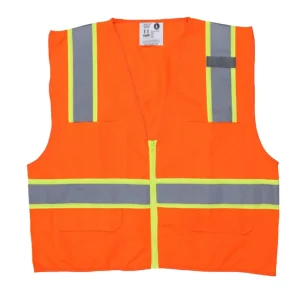
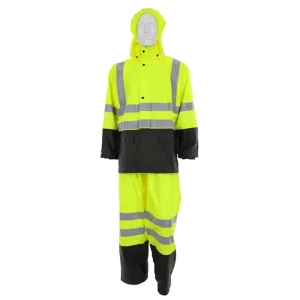
In the modern Australian industrial landscape—spanning the mineral-rich expanses of the Pilbara and Bowen Basin to large-scale urban infrastructure developments like Sydney Metro and Melbourne’s Suburban Rail Loop—personal protective equipment (PPE) has evolved beyond basic body garments. Modern occupational health and safety (OH&S) mandates now recognize high-visibility load-carrying equipment, specifically Hi-Vis Backpacks and Waterproof Hi-Vis Backpack Covers, as critical components of workplace accident prevention visual conspicuity matrices.
For Australian enterprise buyers, procurement managers, and industrial safety distributors, sourcing directly from specialized China Hi-Vis Backpack and Cover factories represents a strategic imperative. This whitepaper analyzes the market drivers, standard compliance metrics (AS/NZS 4602.1:2011, AS/NZS 1906.4:2010), material engineering challenges under extreme UV exposure, and structural advantages provided by Chinese OEM/ODM manufacturing ecosystems in Zhejiang and Jiangsu textile hubs.
Understanding the harsh climatic and regulatory environment in which Australian workers operate.
Australia experiences some of the highest solar UV radiation levels globally. Standard polyester dyes and cheap reflective tapes break down rapidly under Outback sunlight, leading to premature fading (loss of chromaticity) and tape cracking. Chinese factories serving Australia utilize specialized UV-stabilized polymers (UV 400 protected) and colorfast fluorescent dyes (Lime Yellow and Safety Orange) to maintain chromaticity compliance after extended field deployment.
Fly-In Fly-Out (FIFO) mining workers transport delicate electronics, laptops, and safety gear across rugged environments. Industrial backpacks must offer 600D to 1680D Oxford TPU fabric durability, reinforced heavy-duty YKK zippers, dedicated hydration bladder sleeves, and bio-ergonomic load suspension systems, all wrapped in high-conspicuity Class D/N outer shells.
In Northern Queensland and the Northern Territory, monsoonal weather requires 100% waterproof bag protection. Hi-vis waterproof backpack covers with seam-taped 210D Ripstop Nylon or PU coated polyester ensure gear stays bone-dry, featuring elastic drawstring cinches and buckled security straps to prevent covers from stripping off under high winds.
From raw yarn weaving to certified retroreflective heat transfers—unmatched scale and technical mastery.
Chinese safety garment and bag manufacturing facilities possess an unprecedented competitive advantage due to complete vertical integration. Unlike regional assembly workshops, top-tier China Hi-Vis Backpack and cover suppliers control the entire production chain: high-tenacity yarn spinning, waterproof membrane coating, reflective micro-prismatic glass bead application, laser pattern cutting, and automated ultrasonic seam sealing.
Leading Chinese factories offer customized material formulations tailored for Australian tenders. Options include Flame Retardant (FR) Treated 300D Polyester for energy sector workers, Anti-Static (ESD) fabrics for hazardous explosive environments, and GRS-certified Recycled Polyester (rPET) for corporate ESG compliance programs.
Integration of premium glass-bead retroreflective tapes and micro-prismatic vinyl ribbons (certified to AS/NZS 1906.4 Class R & Class RF). Tapes undergo rigorous testing for photometer coefficient of retroreflection ($R_A > 330 \text{ cd/lx}\cdot\text{m}^2$) and maintain performance over 50+ industrial wash cycles.
Full corporate branding capability including screen printing, heat transfer reflective logos, rubber badge applique, and customized zipper pulls. Chinese engineering teams convert Australian client CAD specifications into physical pre-production prototypes within 3-5 business days.
Established export factories operate under strict ISO9001 quality management standards, holding BSCI (Business Social Compliance Initiative), SMETA (SEDEX), and SA8000 certifications to satisfy the stringent corporate governance standards demanded by ASX-listed enterprise buyers.
Technical parameters for procurement teams drafting Australian government and commercial safety tenders.
| Performance Feature | Heavy-Duty Mine Site Hi-Vis Backpack | All-Weather Waterproof Backpack Cover | Australian Compliance Target |
|---|---|---|---|
| Primary Shell Material | 1680D Ballistic Oxford / 600D TPU Coated Polyester | 210D / 190T Waterproof Ripstop Polyester | AS/NZS 1906.4:2010 (High Conspicuity) |
| Fluorescent Chromaticity | Fluorescent Yellow (Safety Lime) / Safety Orange | Fluorescent Lime Yellow / Safety Red-Orange | Class F (Fluorescent Material Standard) |
| Retroreflective Tape | 50mm Class 1 Micro-Prismatic or Glass Bead Taping | 50mm High-Flex Heat Applied Reflective Transfer | Class R / Class RF ($R_A > 330 \text{ cd/lx}\cdot\text{m}^2$) |
| Waterproof Capability | PU/TPU Laminated Membrane (8,000mm Hydrostatic) | PU 10,000mm Taped Seams & DWR Finish | AS 2001.2.17 Water Resistance Test |
| UV & Colorfastness | Grade 4-5 UV Light Fastness (100+ Hours Exposure) | Grade 4-5 UV Protection & Anti-Tear Treatment | AS 2001.4.21 Solar UV Radiation Test |
| Specialized Features | Padded Laptop Bay, Hydration Port, Air-Mesh Backing | 360 Elastic Hem, Bottom Buckle, Stowaway Pouch | Ergonomic Load Distribution & Wind Retention |
Tailored product solutions for specific high-risk operational environments.
Iron ore and lithium extraction sites in the Pilbara mandate strict Class D/N compliance due to heavy vehicle traffic (haul trucks and loaders). Heavy-duty hi-vis backpacks featuring dual high-vis orange/lime panels and 3M Scotchlite reflective taping ensure sub-surface and surface miners remain visible under heavy dust clouds and night illumination.
Organizations such as Sydney Trains, Queensland Rail, and Metro Trains Melbourne require trackside workers to carry safety tools and communications gear in dedicated high-visibility backpacks. Orange hi-vis covers with rail-approved cross-back reflective patterns are compulsory for contract crews working on live rail corridors.
Utility linesmen and remote solar farm technicians traversing rugged terrain benefit from lightweight waterproof hi-vis covers. These covers can be stowed into compact pouches and deployed quickly over standard gear when sudden Outback storms or extreme dust events impair operational visibility.
When establishing direct factory partnerships with Chinese manufacturers, Australian buyers must execute a structured 4-phase sourcing framework to mitigate supply chain risk, guarantee standard compliance, and maximize unit economic margins:
Define exact fabric denier (e.g., 600D Polyester vs 1680D Oxford), backing membrane (PU, PVC, TPU), retroreflective tape certification standards (AS/NZS 1906.4 Class R vs ANSI/ISEA 107), and color Pantone codes for safety lime (Pantone 13-0630 TN) and safety orange (Pantone 15-1360 TN).
Request pre-production samples subjected to third-party lab verification (SGS, Intertek, or TÜV Rheinland). Validate hydrostatic head ratings, tear strength (ISO 13937-2), tensile strength (ISO 13934-1), and retroreflective photometric intensity before signing off on mass production purchase orders (POs).
Implement During Production (DUPRO) and Final Random Inspections (FRI) based on AQL 2.5/4.0 sampling plans. Key inspection parameters include seam tension tests, zipper endurance cycles, waterproof tape seam adhesion, reflective pattern alignment, and packing moisture control.
Optimize shipping volume through vacuum packaging or compressed carton stacking. Ensure accurate tariff classification (HS Code 4202.92 for backpacks / 6307.90 for textile covers) and compliance with Australian Customs commerce marking and country-of-origin labeling regulations.
Partner directly with our specialized manufacturing facility in Zhejiang. We provide fast prototyping, custom OEM branding, and fully certified high-visibility load-carrying solutions tailored to the Australian market.
Send Inquiry Now →Expert answers to key technical, regulatory, and logistics questions from Australian safety distributors.
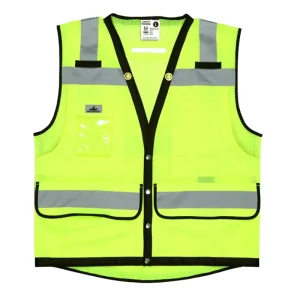
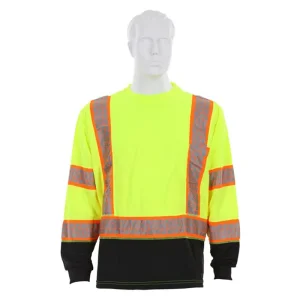
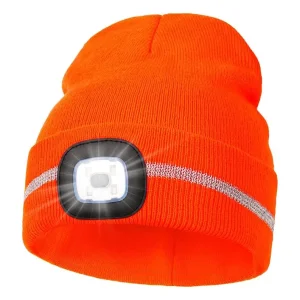
Explore our full line of safety vests, work shirts, rainwear, and high-visibility accessories designed for wholesale distribution.
Contact our dedicated export team today for technical specification consultations, instant wholesale pricing, and sample requests serving Melbourne, Sydney, Brisbane, Perth, and Adelaide.
