Explore our top-certified high-visibility safety clothing, vests, hats, and reflective gear engineered for harsh industrial, construction, and traffic control environments.
An architectural analysis of high-visibility breathable mesh shirts, moisture vapor transport physics, and retroreflective performance under tropical heat stress conditions.
In high-temperature industrial environments such as highway paving, desert mining, maritime logistics, and summer utility maintenance, traditional 100% solid polyester fabrics create a thermal barrier that traps metabolic heat and moisture against the worker's skin. This results in rapid onset heat fatigue, reduced worker vigilance, and non-compliance when workers unbutton or strip off mandated safety apparel.
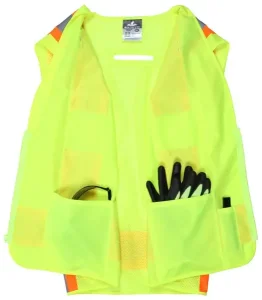
Professional Wholesale Mesh High Vis Shirt Suppliers & Factories solve this physiological challenge by deploying engineered micro-porous synthetic knits—most notably Birdseye Mesh (120 GSM to 160 GSM 100% Polyester) and Piqué Honeycomb Mesh. Birdseye mesh features a specialized geometric knitting pattern that creates thousands of micro-apertures per square meter. These micro-perforations increase air permeability to over 180 cm³/cm²/s (measured via ASTM D737 airflow standard), enabling evaporative cooling through direct cross-breeze airflow while maintaining the mechanical tensile strength needed to hold heavy retroreflective tapes.
Attaching rigid, continuous retroreflective silver bands onto open-mesh knits presents complex engineering challenges: continuous heat-transfer bands can lock the mesh pore structure, reducing breathability along the torso and sleeve lines by up to 35%.
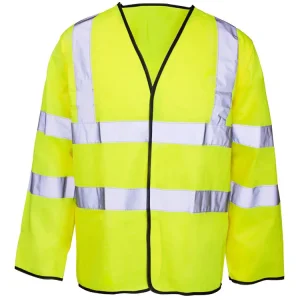
Leading China safety factories overcome this limitation by applying Segmented Heat-Transfer Retroreflective Tape. Rather than a solid foil band, segmented tape consists of micro-patterned retroreflective blocks adhered directly onto individual fabric yarns. This leaves the adjacent mesh micro-pores fully open for unrestricted air movement and 360-degree fabric stretch elasticity. High-performance glass-bead or microprismatic retroreflective films maintain a retroreflection coefficient ($R_A$) exceeding 330 to 500 cd/(lx·m²), exceeding ANSI/ISEA 107 Level 2 brightness requirements even after 50 industrial wash cycles at 60°C.
A clear breakdown of international high-visibility safety requirements for B2B procurement managers, contract specifiers, and OEM brand buyers.
Type R (Roadway) Class 2: Requires minimum 775 sq in. of fluorescent mesh background fabric and 201 sq in. of 2-inch wide retroreflective tape. Ideal for traffic control and construction speeds under 50 mph.
Type R Class 3: Requires 1,240 sq in. of background mesh and 310 sq in. of tape, featuring full-torso coverage with reflective sleeve bands for high-speed highway or night operations.
Harmonized European standard dictating strict chromaticity coordinates ($x, y$) and luminance factors ($\beta \ge 0.70$ for yellow, $\beta \ge 0.40$ for orange).
Class 2 Mesh Shirts: Minimum 0.50m² of background fluorescent mesh and 0.13m² of reflective tape.
Class 3 Mesh Shirts: Minimum 0.80m² background material with continuous reflective bands spanning horizontal torso and vertical shoulders.
Australian and New Zealand standard regulating safety apparel for high-risk environments.
Class D/N (Day/Night): Demands fluorescent hi-vis mesh for high-contrast daytime recognition combined with "H-Pattern" or "X-Pattern" 50mm retroreflective tape for low-light vehicle headlight reflection. UPF 50+ sun protection compliance is frequently required for Australian outdoor mesh shirts.
| Fabric Type | Grammage (GSM) | Air Permeability | Tear Strength | Primary Industrial Application |
|---|---|---|---|---|
| 100% Poly Birdseye Mesh | 120 - 140 GSM | > 210 cm³/cm²/s | High (Spun Filament) | Extreme Heat Construction, Landscaping, Warehousing |
| Piqué Honeycomb Mesh | 150 - 170 GSM | > 165 cm³/cm²/s | Very High (Structured Knit) | Highway Patrol, Airport Apron Crews, Heavy Machinery |
| Tricot Warp Knitted Mesh | 110 - 130 GSM | > 190 cm³/cm²/s | Moderate | Lightweight Safety Vests, Promotional Events |
| FR Treated Modacrylic Mesh | 160 - 190 GSM | > 140 cm³/cm²/s | Superior Fire Retardant | Oil & Gas Operations, Electrical Utilities, Welding |
Why international safety brands, government tender holders, and wholesale distributors trust Yongkang, Zhejiang precision manufacturing for bulk high-visibility shirts.
Every production lot undergoes rigorous multi-tier inspection: raw yarn dye lot color fastness tests, retroreflectivity meter verification, seam burst strength evaluation (ASTM D3786), and final garment measurement audits compliant with ISO 9001 quality systems.
Full custom branding flexibility: silk-screen logo printing, breathable dye-sublimation logos (which keep mesh pores unobstructed), custom woven neck tags, barcoded polybag packaging, radio mic loops, chest pockets, and breakaway velcro side seams.
With 150+ skilled sewing machine operators and automated computerized laser fabric cutters, our 6,000m² facility achieves a monthly production capacity of over 300,000 high-vis garments, delivering seamless container-load shipments to Ningbo and Shanghai ports.
Tailoring high-visibility mesh specifications to distinct physical workplace hazards and climate profiles across global regions.
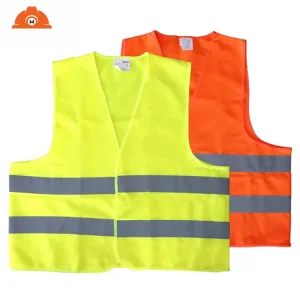
Paving crews operate alongside fast-moving traffic in extreme summer heat. Asphalt ambient temperatures frequently exceed 50°C (122°F). Fluorescent Yellow-Green Mesh High Vis Shirts with 2-inch silver reflective tape deliver high contrast against dark asphalt during daytime while reflecting vehicle headlights from over 300 meters away at night.
Tarmac baggage handlers, fuel truck operators, and aircraft marshals require unrestricted arm movement and rapid heat dissipation. Breathable mesh polo shirts with collar accents, chest pen pockets, and radio mic tabs ensure operational functionality while adhering to FAA and IATA ground safety standards.
High-humidity coastal dockyards demand salt-water resistant fluorescent dyes and anti-microbial mesh fabric treatments. Segmented reflective mesh shirts prevent mold buildup from trapped sweat, providing long-lasting visibility around gantry cranes and container stackers.
Water works, waste management, and electrical grid line workers require high visibility combined with multi-pocket convenience. Dual-tone orange and lime mesh shirts help differentiate worker teams while hiding grime on lower torso panels.
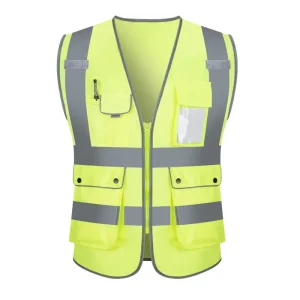
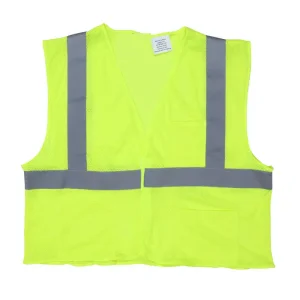
From ultra-lightweight mesh safety vests to heavy-duty waterproof jackets, rainwear, and reflective accessories—a total protective solutions provider.
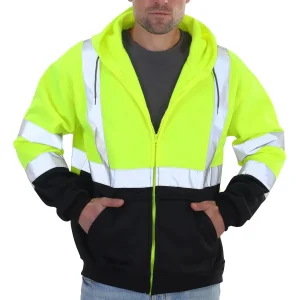
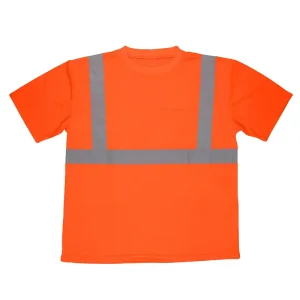
Premium ANSI Class 2/3 reflective shirts, sweatshirts, backpacks, mesh hats, and high-visibility workwear available for global bulk distribution.
Answers to critical questions regarding GSM weights, customization limits, certification compliance, and factory lead times.
For tropical or summer work environments (above 35°C / 95°F), we recommend a 120 GSM to 130 GSM 100% polyester birdseye knit. This weight provides ideal airflow and quick evaporation without sacrificing tear strength. For industrial environments with high abrasion risks, 150 GSM mesh offers greater mechanical durability while remaining significantly cooler than 200+ GSM solid tricot fabrics.
Yes, if not properly calculated. Screen printing thick plastisol inks covers the fluorescent mesh background material. If the total unprinted fluorescent area drops below ANSI Class 2 (775 sq in.) or Class 3 (1,240 sq in.) limits, compliance is voided. We utilize breathable dye-sublimation printing or place logos on non-certified chest pockets or sleeves to guarantee full standard compliance.
Solid reflective tape is stitched onto the garment, which can constrict fabric stretch and cover mesh ventilation pores along the chest and back. Segmented reflective tape is heat-transferred in individual geometric blocks, allowing the mesh fabric underneath to breathe, stretch, and flex naturally with the worker's movements.
Our standard MOQ is 500 pieces per style/color for custom OEM orders with branded labeling, logo printing, and custom packaging. Production turnaround is typically 15 to 25 days following sample approval. For ready-to-ship stock items, smaller trial quantities can be dispatched within 5 to 7 business days.
Our in-house QA lab uses calibrated retroreflectometers to ensure every batch of silver glass-bead tape meets or exceeds 330 cd/(lx·m²). We perform accelerated industrial laundering tests according to ISO 6330 standards, verifying that reflectivity remains compliant above 100 cd/(lx·m²) after 25 to 50 wash cycles.
Yes. We produce high-density birdseye mesh variants specifically engineered to block harmful ultraviolet rays, achieving UPF 30+ to UPF 50+ ratings certified under AS 4399 standards while retaining mesh air permeability for hot Australian mining and construction sites.