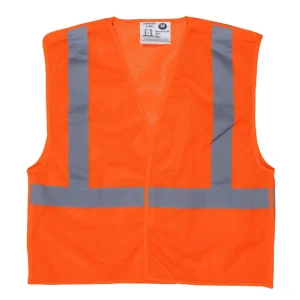
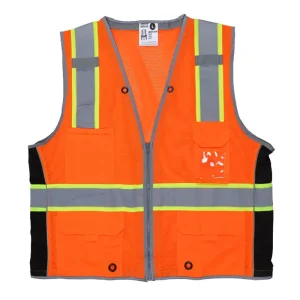
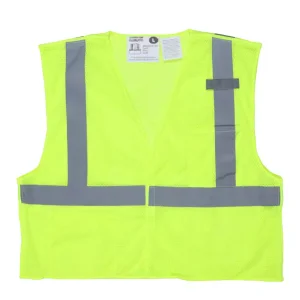
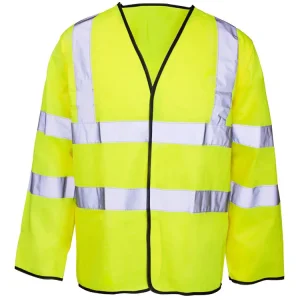
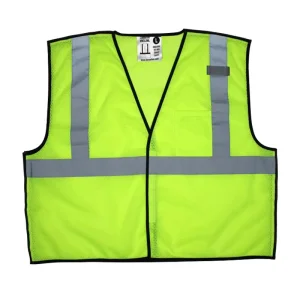
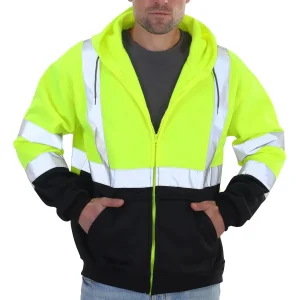
Factory-direct OEM/ODM solutions engineered for extreme durability, regulatory compliance, and precision logo branding.
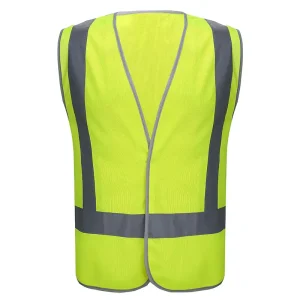
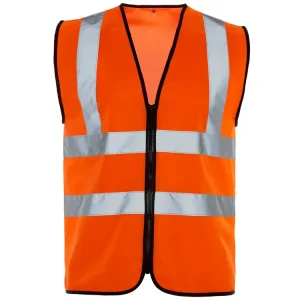
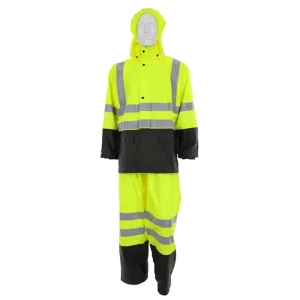
In modern industrial procurement, the strategic integration of customized corporate logos onto high-visibility (hi-vis) safety jackets has evolved far beyond basic aesthetics. Today’s global enterprise buyers, Occupational Health and Safety (OHS) managers, and industrial equipment distributors face a dual imperative: maintaining uncompromising compliance with stringent international PPE mandates while projecting unified corporate identity across high-risk operational sites.
Selecting certified China safety jacket logo manufacturers and suppliers requires deep operational scrutiny. China’s advanced textile manufacturing hubs—most notably in Zhejiang and Jiangsu provinces—have undergone a technological revolution. By combining high-precision automated embroidery, eco-solvent screen printing, laser-cut reflective heat transfer film, and ultra-durable background fabric engineering, tier-1 Chinese manufacturers provide global supply chains with an unbeatable balance of cost efficiency, scalability, and technical compliance.
Navigating global supply chain volatility, compliance risks, and technical customization demands.
Improper logo application can obscure minimum required fluorescent fabric surface area, invalidating ANSI/ISEA 107-2020 or EN ISO 20471 certifications. Our engineering process mathematically recalculates background fabric ratios prior to printing, guaranteeing total site compliance.
Leveraging fully automated cutting beds, multi-head computer embroidery systems, and continuous-roll heat transfer presses, leading Zhejiang suppliers offer rapid prototyping alongside high-volume production runs exceeding 500,000 units monthly.
From DDP (Delivered Duty Paid) shipping solutions for regional safety equipment suppliers to localized customs documentation assistance, top Chinese safety jacket suppliers eliminate import friction across EU, NA, and APAC trade corridors.
Analyzing retroreflective coefficient retention, chemical adhesion durability, and fabric printability.
The application of corporate logos onto safety jackets is not merely a graphic process; it is a polymer adhesion challenge involving complex fabric treatments. High-performance safety jackets are routinely finished with DWR (Durable Water Repellent) coatings, PU/TPU breathable laminations, or flame-retardant chemical baths. Applying logos without compromising technical performance requires precise method selection:
Ideal for large-volume orders on 100% polyester mesh or solid woven fabrics. Utilizes specialized plastisol or eco-friendly water-based polyurethane inks formulated with cross-linking agents to ensure adhesion to hydrophobic surfaces.
Engineered by embedding high-index glass beads (refractive index $n \ge 1.93$) or micro-prismatic structures directly into thermal adhesive TPU films. The logo itself shines bright retroreflective light back to vehicle headlights.
Selected for premium executive safety parkas, softshell jackets, and supervisor winter coats. Uses colorfast 100% polyester yarns that resist UV degradation and chemical fading.
Sublimation embeds disperse dyes directly into polyester fibers at $200^\circ\text{C}$, maintaining complete fabric breathability without adding surface weight. Vulcanized rubber/PVC patches are used for rugged outdoor environments.
| Logo Printing Methodology | Retroreflectivity ($R_A$) | Wash Fastness (ISO 6330) | Waterproof Impact | Optimal Application Zone |
|---|---|---|---|---|
| Reflective Thermal Film | Very High (> 400 cd/lux) | 25–50 Cycles | Zero Impact | Upper Back / Chest Pocket |
| Screen Printing (Polyurethane Inks) | None (Standard Tint) | 50+ Cycles | Zero Impact | Full Back / Sleeves |
| Sealed Computer Embroidery | N/A (Yarn Based) | 75+ Cycles | Requires Seam Tape | Left Chest Badge Area |
| Sublimation Printing | None (Fiber Level) | 100+ Cycles | Zero Impact | Breathable Mesh Vests |
Vertical integration, raw material supply chain dominance, and stringent Quality Assurance (QA/QC) benchmarks.
China’s role as the primary global hub for high-visibility personal protective equipment (PPE) manufacturing stems from its fully integrated industrial chain. From raw PET chip synthesis and filament spinning to fluorescent dyeing, retroreflective tape manufacturing, and final automated garment assembly, Chinese manufacturers offer unrivaled operational control.
Yongkang and the broader Zhejiang safety gear manufacturing cluster maintain direct access to specialized weaving mills producing 120gsm to 300gsm polyester mesh, oxford weaves, and 3-layer softshell laminates. This vertical link guarantees seamless color-matching to international Pantone safety standards (Fluorescent Yellow-Green 13-0630 TN, Fluorescent Orange-Red 16-1359 TN).
Leading Chinese exporters maintain accredited testing laboratories equipped with retroreflectometer testing devices, hydrostatic head pressure testers, and spectrophotometers. Every batch of custom logo-printed safety jackets undergoes rigorous testing to verify initial retroreflective luminance ($R_A$) and color chromaticity coordinates ($x, y$) after customized logo application.
With digital vector file processing and automated digital sample cutting tables, tier-1 suppliers convert buyer artwork files into physical logo-printed pre-production samples within 24 to 48 hours, significantly accelerating international procurement cycles and tender bidding timelines.
Preventing compliance failures caused by incorrect logo sizing, tape obstruction, or non-certified ink usage.
A critical challenge when ordering safety jackets with custom logos is ensuring that branding elements do not breach international high-visibility safety standards. Standards such as ANSI/ISEA 107-2020 (USA), EN ISO 20471:2013+A1:2016 (Europe), and AS/NZS 4602.1:2011 (Australia/New Zealand) dictate strict geometric surface area minimums for both background fluorescent material and retroreflective tape.
Class 2 & Class 3 Requirements: ANSI Class 2 requires a minimum of $775 \text{ in}^2$ ($0.50 \text{ m}^2$) of background fabric, while Class 3 requires $1240 \text{ in}^2$ ($0.80 \text{ m}^2$).
Class 1, 2, and 3 Hierarchy: Enforces mandatory 360-degree torso coverage with vertical or horizontal bands of reflective material.
NFPA 2112, EN 1149 (Anti-Static & FR): Offshore oil rigs and utility sub-stations require flame-retardant (FR) and anti-static hi-vis outerwear.
Tailoring safety outerwear solutions to harsh, specialized working environments.
Workplace conditions involve high dust, heavy machinery friction, and continuous daytime/nighttime traffic exposure. Safety vests and bomber jackets require high-durability 300D Oxford fabric with waterproof PU backing.
Logo Strategy: Large, bold block-letter screen printing on the upper back using polyurethane-based inks. High contrast ensures instantly recognizable corporate branding for site safety compliance officers and passing motorists.
Ground crews work near jet engine exhaust streams and low-light tarmac environments. Non-magnetic, dielectric plastic zipper closures are essential to eliminate FOD (Foreign Object Debris) risks and electrical hazards.
Logo Strategy: Silver retroreflective film logos applied to the left chest and back. High coefficient retroreflection guarantees instant illumination under mobile airfield spotlights and aircraft taxiing lights.
Extremely hostile marine environments with heavy exposure to saltwater, hydrocarbon oils, and extreme climate changes. Outerwear requires multi-norm certification (EN ISO 20471, EN 343 waterproofness, EN ISO 11612 flame protection).
Logo Strategy: Flame-retardant heat transfer films or Nomex® embroidered badges stitched with Kevlar® threads onto reinforced chest panels, maintaining structural durability under high chemical exposure.
High-frequency operational movement within temperature-controlled fulfillment centers. Workwear emphasizes thermal comfort, lightweight stretch fabrics, and ergonomic body-mapped fit.
Logo Strategy: Sublimated printing or high-density silicone transfer badges on breathable mesh fabrics. Allows corporate branding while retaining full stretch performance and moisture-wicking properties.
Smart PPE integration, eco-friendly sustainable fabrics, and bio-based reflective coatings.
Top Chinese manufacturers are pioneering 100% recycled polyester (rPET) hi-vis fabrics derived from post-consumer plastic bottles. Combined with water-based, solvent-free printing inks, these eco-conscious safety jackets enable global corporations to meet strict Scope 3 ESG carbon-reduction goals without compromising technical performance.
Moving beyond passive retroreflection, next-generation safety jackets integrate flexible, washable active LED strip lights powered by lightweight rechargeable lithium polymer battery packs. Logos are surrounded by micro-LED perimeter fiber optics, providing self-illuminating visibility in complete darkness or thick smoke.
Integrating washable, high-frequency RFID chips and encrypted NFC antenna tags directly into silicone corporate logo patches. Enables automated asset tracking, personnel access control at industrial job sites, and real-time laundering cycle tracking for fleet safety gear management.
Addressing key operational, technical, and regulatory procurement questions for global buyers.
High-visibility vests, weather-proof outerwear, surveyor equipment, and night-safety headwear.