Explore our industrial-grade protective apparel engineered for global safety compliance, maximum daytime luminescence, and nighttime retroreflectivity.
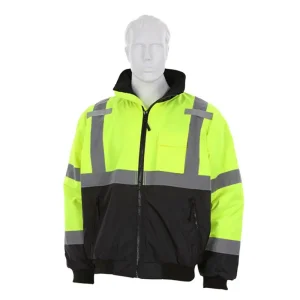
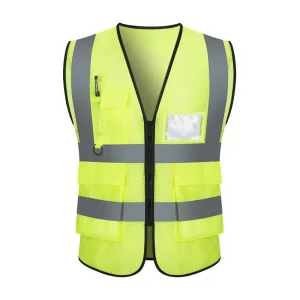
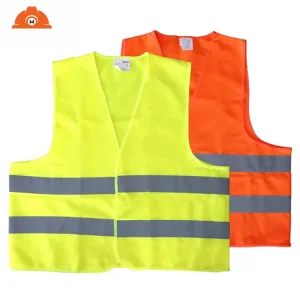
In the modern industrial safety environment, high-visibility apparel is no longer evaluated solely by visual compliance; ergonomic physiology, thermal regulation, micro-climate moisture transport, and arc-flash resistance have become critical procurement metrics.
Historically, high-visibility workwear relied almost exclusively on 100% synthetic polyester textiles due to the chemical ease of bonding fluorescent dyes (such as solvent-based yellow, orange-red, and pink) to hydrophobic synthetic fibers. However, prolonged exposure to harsh environmental conditions, intense physical exertion in mining and construction sites, and volatile petrochemical facility work environments highlighted severe thermal and physiological limitations of pure polyester garments.
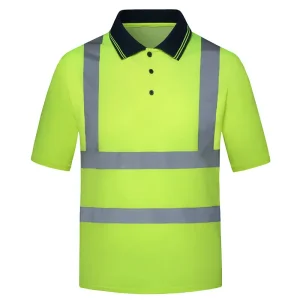
As leading global regulatory bodies—including OSHA (USA), Safe Work Australia, and the European Agency for Safety and Health at Work (EU-OSHA)—tighten workplace welfare standards, global B2B buyers are actively transitioning toward high-vis cotton polo shirts. Natural cotton and cotton-rich blends offer unparalleled sweat absorption, reduction of skin contact heat stress, anti-static properties, and inherent flame resistance when treated, fulfilling the dual requirements of occupational safety compliance and long-shift wearer comfort.
The global high-visibility workwear market is experiencing a profound architectural shift driven by three primary commercial catalysts: ESG (Environmental, Social, and Governance) corporate mandates, micro-climate thermal engineering, and strict regional safety standardization.
Operated heavily across Western Australia, Chile, and Southern Africa. Requirements emphasize high-grammage (200-240 GSM) 100% cotton pique fabric that prevents soil ingress while providing natural UV protection (UPF 50+) and breathability during extreme ambient heat (exceeding 40°C).
Rapid automation across North America and Europe requires workers operating alongside AGVs (Automated Guided Vehicles) to wear high-mobility, stretchable cotton-rich polo shirts featuring micro-segmented retroreflective tape that accommodates continuous torso rotation.
Utilities demand cotton workwear to prevent synthetic melting injuries caused by electric arc flashes. Non-melting natural cotton combined with static-dissipative carbon yarns represents the gold standard for high-voltage maintenance crew polo uniforms.
The primary historical obstacle in manufacturing cotton hi-vis polo shirts was the cellulosic molecular structure of cotton. Unlike polyester, which absorbs hydrophobic disperse dyes deep within its polymer matrix under high heat, natural cotton fibers possess hydroxyl groups that traditionally struggled to bind high-luminescence fluorescent yellow (Fluorescent Yellow Green) and fluorescent orange-red dyes with sufficient color fastness.
By blending long-staple combed cotton (60%-80%) with high-density polyester microfibers (20%-40%), our engineering team crafts a dual-face plated fabric. The interior skin-contacting layer consists of 100% natural soft cotton fibers for maximum wicking, while the exterior facing layer utilizes micro-polyester filaments optimized for reactive fluorescent dye binding. This guarantees compliance with EN ISO 20471 chromaticity coordinates (x, y) and brightness luminance factor (β ≥ 0.70 for yellow).
Traditional continuous solid retroreflective glass-bead tapes create thermal barrier zones across the chest and back, causing sweat entrapment. Modern China Factory 4.0 production integrates micro-segmented heat-transfer tape. Composed of thousands of wide-angle retroreflective glass beads embedded in a flexible polymer base, these segmented strips allow total fabric breathability, dynamic 4-way stretch compliance, and zero tape cracking after 50+ rigorous industrial laundering cycles at 60°C.
| Performance Specification | 100% Combed Cotton Hi-Vis | CVC Cotton/Poly Blend (60/40) | 100% Polyester Mesh/Pique |
|---|---|---|---|
| Skin Thermal Comfort & Breathability | Exceptional (Natural absorption) | High (Plated sweat-wicking structure) | Moderate to Low (Can retain body odor) |
| Color Fastness to UV / Wash | Grade 4.0 (Requires specialized reactive dyes) | Grade 4.5+ (Superior color holding) | Grade 5.0 (Optimal dye retention) |
| Tensile & Bursting Strength | High (220-240 GSM Pique) | Very High (Poly-reinforced core) | Moderate (Prone to snagging) |
| Arc Flash & Anti-Static Performance | Inherently Safe / Non-Melting | Good (Passes standard industrial thresholds) | Poor (Melts under extreme heat exposure) |
| Standards Compliance | ANSI Class 2 / EN ISO 20471 | ANSI Class 2 & 3 / EN ISO 20471 | ANSI Class 2 & 3 / EN ISO 20471 |
Sourcing high-visibility cotton polo shirts from premium Chinese manufacturers offers global enterprise buyers strategic cost benefits, cutting-edge automated quality control, and robust supply chain resilience.
Utilizing CAD-integrated automated spreading and laser cutting machinery ensures dimensional tolerance precision within ±1mm across tens of thousands of garments, preserving precise collar alignment and seamless reflective tape pattern matching.
Every fabric batch undergoes rigorous spectrophotometer color measurement under daylight, fluorescent, and incandescent light sources to eliminate lot-to-lot shade variation and guarantee exact compliance with international chromaticity boundaries.
From spinning raw long-staple cotton yarn in Zhejiang industrial textile hubs to automated knitting, eco-friendly piece dyeing, reflective film laminating, and direct port shipment—our integrated cluster minimizes production lead times by up to 35%.
High-visibility cotton polo shirts are deployed across diverse micro-environments globally. Engineering specifications must adapt to climate factors, site-specific hazards, and corporate branding protocols.
Environment: Intense UV exposure, high humidity, ambient temperatures exceeding 45°C.
Technical Configuration: 180 GSM lightweight 100% cotton pique, anti-UV treatment (UPF 50+), ventilated underarm eyelets, high-contrast lime-yellow base fabric with perforated 3M retroreflective tape to facilitate maximum skin heat release.
Environment: Fast-paced tarmac operations requiring strict compliance with EN ISO 20471 Class 2/3.
Technical Configuration: 220 GSM CVC cotton-poly polo shirt with rib-knit collar, integrated radio/mic loops, reinforced pen pockets on sleeves, custom corporate logo embroidery with fire-retardant backing thread.
Environment: Heavy dust, volatile chemical exposure, mandatory daytime/nighttime AS/NZS 4602.1:2011 compliance.
Technical Configuration: Heavyweight 240 GSM pre-shrunk cotton polo with navy blue lower body panels to conceal dirt and grease, equipped with dual-hoop retroreflective tape pattern across the torso and arms.
Environment: Urban roadside inspection, traffic control, and municipal utility repair.
Technical Configuration: ANSI/ISEA 107-2020 Type R Class 2 certified cotton polo shirt with breakaway side seam zippers, moisture-wicking antimicrobial finish, and dynamic heat-applied stretch reflective striping.
Find authoritative answers regarding standards compliance, manufacturing capabilities, material selections, and bulk purchasing parameters.
Discover our specialized factory-direct safety garments, weather-proof outerwear, and high-visibility accessories designed for worldwide distribution.