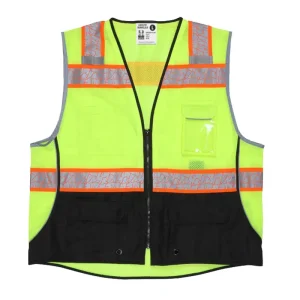
Precision-manufactured high-visibility apparel and tactical workwear engineered to meet strict international safety parameters.
Bridging executive aesthetics, high-stain resistance, and multi-hazard compliance across modern industrial environments.
Historically, industrial safety compliance dictated fluorescent neon yellow and orange-red as the sole standards for personal protective equipment (PPE). However, modern occupational security, corporate logistics management, site supervision, and event management require a balance of stain concealment, professional hierarchy, and high contrast optical reflectivity. Premium black safety vests engineered by top China suppliers have emerged as an essential solution for environments where heavy oil, grease, and dirt render conventional fluorescent vests prematurely dirty, thereby lowering total cost of ownership (TCO) while enhancing worker authority.
Black safety vests manufactured to ANSI/ISEA 107-2020 Type O (Off-road) or Class 1 / Class 2 standards utilize dual-tone trim architecture. By layering high-grade micro-prismatic silver retroreflective tape over high-visibility fluorescent yellow or lime background fabric ribbon, black vests deliver extraordinary optical pop during both daytime and low-light operations. This technical design ensures that light emitted from vehicle headlights is focused directly back to the driver's line of sight, preserving vital reaction times in high-risk zones.
China accounts for over 65% of global high-visibility garment manufacturing. Concentrated hubs such as Yongkang in Zhejiang Province leverage vertically integrated supply chains—from fiber extrusion, warp knitting, and retroreflective bead coating to automated CAD pattern cutting and precision stitching. Enterprise buyers collaborating directly with established China black safety vest factories achieve unmatched OEM customization flexibility, rapid sampling cycles, and compliant mass manufacturing at scale.
Analyzing why Fortune 500 fleets, security agencies, and construction conglomerates are expanding black vest specifications.
When B2B procurement managers, safety directors, and corporate buyers query "China Black Safety Vest Suppliers & Factories", their search intent encompasses far more than simple transactional price checks. It reflects a multi-dimensional procurement evaluation involving ergonomic durability, regulatory compliance, branding customization, and supply chain reliability. Modern industrial operations present diverse operational requirements that black safety vests solve with exceptional effectiveness:
Forklift operators, yard marshals, and last-mile delivery crews are exposed to grease, exhaust soot, and mechanical friction. High-visibility yellow vests often become dirty within weeks, requiring replacement or harsh industrial laundering that degrades retroreflective performance. Black bottom and full-black safety vests maintain a sharp, clean corporate image while retaining critical visibility trims, significantly lowering annual gear replacement budgets.
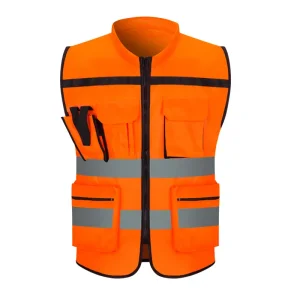
Tactical security officers, event crowd managers, and emergency response teams require an authoritative uniform that commands respect while keeping personnel visible in dense crowds or low-light venues. Black surveyor safety vests equipped with multi-functional radio loops, clear ID badge windows, and heavy-duty zippers offer the ideal balance of tactical utility and reflective safety.
On large-scale civil engineering, infrastructure, and mining construction sites, differentiating site supervisors, project managers, and safety inspectors from general labor crews is vital for operational efficiency and emergency response. Black surveyor executive vests serve as visual markers of leadership while maintaining site safety compliance.
A granular breakdown of textile technology, optics chemistry, structural reinforcement, and smart garment evolution (2025–2030).
| Engineering Module | Current Market Benchmark | Advanced OEM Technical Specification | Future Technology Roadmap (2025-2030) |
|---|---|---|---|
| Base Fabric Composition | 100% 110 GSM Plain Knit Polyester | 120-150 GSM High-Tenacity Warp Knit Mesh / 300D Oxford with DWR (Durable Water Repellent) finish | Recycled rPET GRS-Certified Fibers with Anti-Static Carbon Thread & Flame Retardant (FR) Inherent Weaves |
| Retroreflective Optics | Standard Class 2 Glass Bead Sewn Tape (330 cd/lux) | Dual-Tone High-Gloss Micro-Prismatic Tape / 3M™ Scotchlite™ 8912 Thermal Transfer Film (≥500 cd/lux) | Segmented Heat-Applied Elastic Reflective Strips with Flexible Photoluminescent Glow-in-the-Dark Polymers |
| Closure & Structural Hardware | Standard Nylon Coil #3 Zipper | Reinforced #5 Resin Heavy-Duty Dual Zipper with Corrosion-Resistant Brass/Plated Zinc Sliders | Magnetic Quick-Release Auto-Lock Fasteners & Emergency Breakaway Snap Systems |
| Color Fastness & Laundering | Grade 3-4 (15 Wash Cycles at 40°C) | Grade 4-5 Color Fastness to Rubbing/Light (50+ Industrial Wash Cycles at 60°C ISO 6330) | Nanotech Stain-Repellent Coating (Oleophobic & Hydrophobic) with Zero Degradation Reflective Tape |
| Functional Ergonomics | Basic 2 Pocket Layout | 6 to 9 Pocket Surveyor Layout: Padded Tablet Pocket, Mic Tabs, D-Ring Port, Reinforced PVC ID Card Holder | Integrated IoT Wearable Sensor Sleeves (H2S Gas Detection, GPS Beacon, Body-Heat Thermal Monitoring) |
The core performance of any black safety vest relies on retroreflective technology. Unlike diffuse reflection (which scatters light in all directions) or specular reflection (like a mirror), retroreflective materials redirect light back along the vector of incidence. China leading factories deploy millions of microscopic wide-angle glass beads (refractive index n ≥ 1.90) embedded within a durable polymer matrix. When vehicle headlights strike the tape, light is refracted, reflected off a back mirror coating, and sent straight to the driver's eyes—transforming a stealthy black garment into a highly visible beacon at night.
For B2B buyers, product lifespan directly dictates ROI. Top suppliers in Yongkang conduct rigorous laboratory testing on black safety vests. Fabrics undergo ISO 13934-1 tensile strength testing to ensure seams do not tear under stress. Reflective trims are subjected to accelerated weathering and 50+ wash cycles under ISO 6330 standards. High-tier black safety vests retain minimum retroreflectivity values exceeding 100 cd/(lx·m²) even after prolonged industrial wash routines, guaranteeing worker safety over long service periods.
A black background provides an exceptionally sleek canvas for corporate identity. Chinese suppliers offer advanced decoration technologies tailored to complex logos: Silkscreen printing with Plastisol inks for crisp opacity; high-density computer embroidery for executive aesthetics; heat-transfer vinyl (HTV); and reflective logo transfer film that shines bright alongside safety tapes under night illumination.
Ensuring full market accessibility and workplace safety compliance across North America, Europe, Australia, and Asia-Pacific.
Importing high-visibility safety clothing requires strict compliance with destination market standards. Failure to meet these regulations can lead to customs seizures, municipal fines, or compromised worker safety. A knowledgeable OEM factory partner guides procurement clients through precise fabric, color, and tape coverage requirements:
Under American National Standard for High-Visibility Safety Apparel, full black vests are typically classified under Type O (Off-Road), Class 1. For applications requiring Class 2 or Class 3 compliance, China suppliers construct "Enhanced Visibility" dual-tone black vests featuring fluorescent yellow/orange accent panels with minimum required background material areas (0.50 m² for Class 2) combined with 217 sq. inches of retroreflective tape.
The European standard EN ISO 20471 enforces strict chromaticity coordinates and luminescence factors for background materials. While pure black fabric cannot qualify as EN ISO 20471 certified background fabric on its own, supplier factories produce RIS-3279-TOM compliant dual-tone garments (popular in UK rail and construction) where black lower-body panels mask dirt while the upper torso meets Class 2 fluorescent orange guidelines.
The Australian and New Zealand market requires compliance with AS/NZS 1906.4 (High-visibility materials) and AS/NZS 4602.1 (Garments for high risk applications). Class D/N (Day/Night) black safety vests incorporate specialized "H-pattern" or "X-pattern" rear reflective striping with side breakaway features tailored to local mining and forestry regulations.
Empowering global brands, distributors, and safety equipment wholesalers with high-capacity OEM & ODM production solutions.
Headquartered in Jinhua City, Zhejiang, Yongkang Wow Safety Products Co., Ltd. operates a state-of-the-art 6,000 m² manufacturing plant staffed by 150+ skilled textile technicians. Equipped with automated fabric laser cutters, computerized pattern sewing machines, and automatic heat-press transfer lines, the plant achieves a monthly output exceeding 400,000 safety garments.
Quality assurance is embedded in every stage of manufacturing. Raw fabric rolls undergo spectrophotometric color consistency checks and GSM density weighing. Reflective tapes undergo retroreflection testing using handheld retroreflectometers prior to cutting. Final garments are subjected to 100% thread trimming, zipper endurance testing, and random AQL 2.5 sampling before export packaging.
With 15+ years of international export experience across 50+ countries, Wow Safety offers complete end-to-end B2B services—including custom artwork proofing, specialized barcoding, retail hangtag design, export customs documentation, and flexible Incoterms (FOB Ningbo/Shanghai, CIF, DDP to client fulfillment centers).
Clear, authoritative technical answers to common questions raised by global enterprise safety buyers.
A standard full-black fabric vest cannot achieve Class 2 certification independently because ANSI/ISEA 107-2020 mandates a minimum of 775 square inches of certified high-visibility fluorescent background fabric (lime-yellow, orange-red, or red). However, black vests can qualify under ANSI Type O, Class 1 for off-road use. Alternatively, dual-tone black vests—which combine fluorescent lime panels over the shoulders and chest with a black lower torso—can fully meet ANSI Class 2 requirements while offering stain-concealment benefits.
For standard stock models with custom logo screen-printing, our MOQ starts at just 500 units. For fully customized OEM orders—including custom fabric dyeing (Pantone matching), bespoke pocket dimensions, custom zipper pulls, and private labeling—our typical MOQ is 1,000 to 2,000 units per style, allowing for maximum cost efficiency.
We recommend high-density Plastisol Silkscreen Printing with a white underbase, or Reflective Thermal Transfer Vinyl. The underbase prevents the dark black mesh fabric from bleeding through lighter ink colors, preserving vibrant corporate logos. Reflective heat-transfer logos provide double duty by enhancing nighttime branding visibility.
Custom physical samples are developed and dispatched within 5 to 7 business days following artwork confirmation. Once mass production samples are approved and deposit is received, standard manufacturing delivery times range from 20 to 30 days, depending on overall order volume and custom material requirements.
While dark fabrics absorb more solar heat than fluorescent yellow, our black safety vests utilize specialized 100% open-weave polyester bird's-eye or honeycomb mesh (120-140 GSM). This allows maximum airflow and rapid heat dissipation, keeping workers cool in warm outdoor environments.
Explore our full line of reflective headwear, protective gaiters, and specialized safety accessories.